Benfotiamine Powder
Description
Benfotiamine Powder 98% HPLC – Fat-Soluble Vitamin B1 Derivative for Advanced Nutritional Formulations
Xi'an Le-Nutra Ingredients Inc supplies premium-grade Benfotiamine Powder with guaranteed ≥98% purity verified by HPLC, manufactured at our certified 60,000㎡ production facility with 3,000-ton annual capacity. Unlike water-soluble thiamine, our product offers superior lipid solubility and cellular bioavailability, solving critical formulation challenges in metabolic support supplements and functional nutrition products. Each batch undergoes rigorous quality control including heavy metal screening (Pb<10ppm, As<2ppm), microbial testing (TPC≤1000 CFU/g), and moisture analysis (≤0.5% loss on drying) to ensure consistent pharmaceutical-grade quality across all shipments.
What Is Benfotiamine Powder?
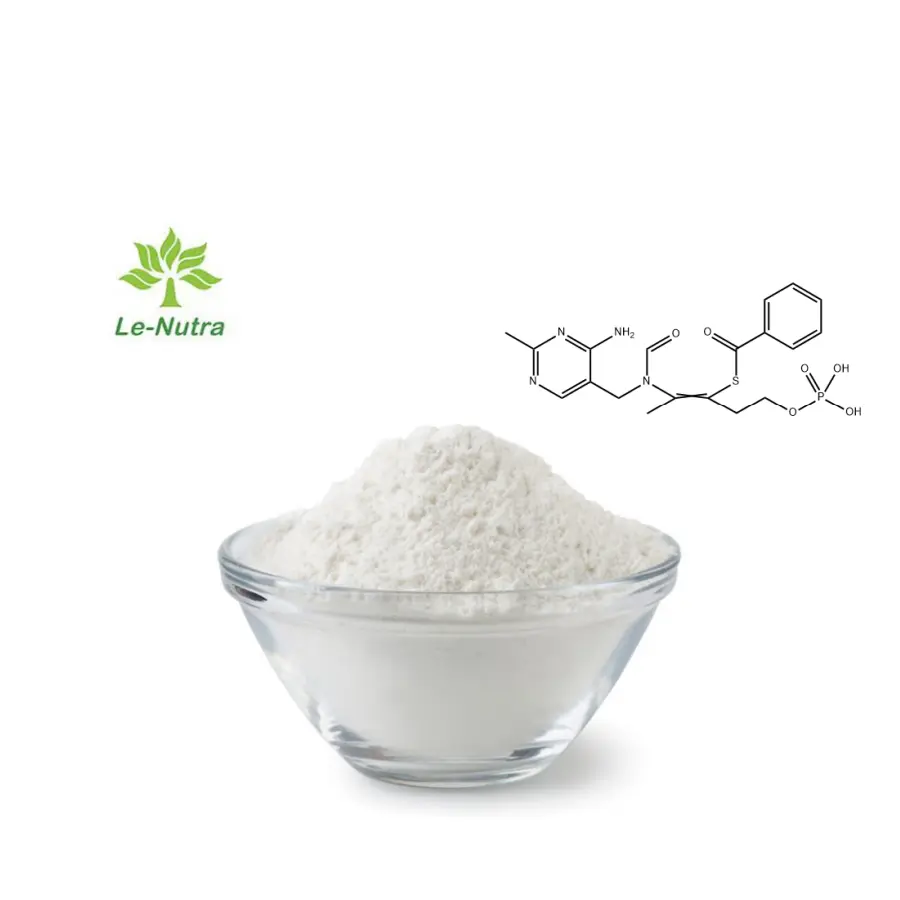
Benfotiamine is a synthetic derivative of thiamin (Vitamin B1). Chemically, it has an open thiazole ring structure and is synthesised via S-acylation modification of thiamin. This chemical engineering converts the hydrophilic vitamin into a lipophilic molecule with a dramatically improved membrane permeability.
The chemical is a free-flowing crystalline powder, off-white in colour, CAS No 22457-89-2, soluble in oils and heated ethanol. Its unique lipid-soluble profile allows for a better intestinal uptake than standard thiamin supplements, which have a poor bioavailability due to saturable active transport mechanisms.
This ingredient addresses the big problem of providing adequate thiamin nutrition without excessive dosage or dosing frequency to manufacturers of metabolic health products.
Technical Specifications and Quality Standards
| Item | Specification |
|---|---|
| Product Name | Benfotiamine Powder 98% |
| CAS Number | 22457-89-2 |
| Source | Chemical synthesis with recrystallization purification |
| Active Ingredient | Benfotiamine |
| Appearance | Off-white free-flowing crystalline powder |
| Assay | ≥98.0% HPLC |
| Solubility | Soluble in oil, slightly soluble in warm ethanol |
| Loss on Drying | ≤0.5% |
| Total Ash | ≤0.1% |
| Heavy Metals | Pb<10ppm, As<2ppm, Cd<1ppm, Hg<0.1ppm |
| Microbial Limits | TPC≤1000 CFU/g; Yeast & Mold≤100 CFU/g |
| Pathogen Testing | E. coli & Salmonella: Negative |
| Storage Conditions | Sealed, light-protected, cool & dry environment |
| Shelf Life | 24 months under proper storage |
Core Functional Advantages for Product Development
Optimised Fat-Soluble Thiamin Nutrition
The lipophilic structure bypasses the rate-limiting intestinal thiamin transporters achieving blood plasma concentrations 5-25 times greater than equal doses of water soluble thiamin. This leads into better cellular absorption and sustained intracellular availability of thiamin.
Support for Balanced Carbohydrate Metabolism
After absorption, benfotiamine is converted to thiamin pyrophosphate (TPP), the active coenzyme needed for the activity of pyruvate dehydrogenase and alpha-ketoglutarate dehydrogenase. The biochemical route is suitable for efficient exploitation of glucose and energy generation at mitochondrial level.
Peripheral Circulatory Comfort Preservation
Clinical research studies have demonstrated that benfotiamine activates transketolase enzymes that divert glycolytic intermediates from routes of advanced glycation end-product (AGE) production . This system gives functional support to pleasant peripheral nerve and vascular function.
Comprehensive Daily Vitamin Supplementation
Good for use in multivitamin formulas, metabolic health blends and specialised nutritional support solutions. Benfotiamine Powder is flexible in its use in multiple administration modalities such as tablets, capsules and oil based solutions.
Manufacturing Excellence and Production Capability
Our 60,000㎡ GMP-certified facility has 6 multipurpose manufacturing lines and the most advanced recrystallisation purification equipment. Production cycles are carried out under tight pharmaceutical grade regulations and include in-process quality inspections.
The expert R&D team is constantly optimising the process to ensure that the particle size is consistent and has great flowability for automatic encapsulation equipment. We maintain over 30 days of safety stock and have global logistical agreements that allow us to achieve 98% on-time delivery.
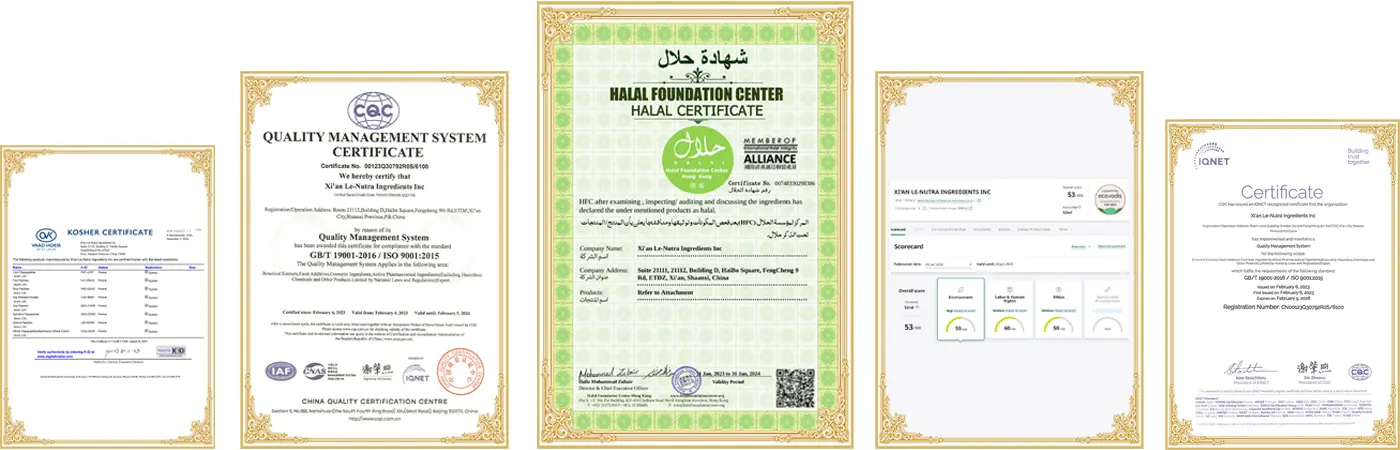
All batches are validated via third-party testing. Full paperwork including FDA compliance, ISO certification, GMP audit reports, Kosher certification, COA, TDS, MSDS and MOA is available upon request.

Versatile Applications Across Formulation Categories
Softgel Encapsulation Technology
Its oil-soluble feature makes it suitable for softgel formulations with medium-chain triglycerides or vegetable oils. We can vary the fineness of the particle as your filling equipment requires.
Compression of Multi-Vitamin Tablet
It is suitable for direct compression and wet granulation tablet technique. Low moisture level (≤0.5 %) minimises caking during storage and gives tableting flow characteristics.
Metabolic Support Mixture Capsules
Works in conjunction with alpha-lipoic acid, chromium picolinate and B-complex vitamins in specialised metabolic health formulas to enhance glucose metabolism.
Nutritional Drinks (Oil Suspension)
Low solubility in warm ethanol enables functional ingredient inclusion into beverage emulsion systems, giving a new delivery method for liquid nutrition products to manufacturers.
Complete Quality Assurance Protocol
Each production batch is extensively quality validated through a variety of analytical techniques. HPLC analysis shows ≥98% active ingredient purity with specified retention time coinciding with reference standards.
ICP-MS analysis is conducted for heavy metals screening to confirm compliance with international food safety guidelines. Microbiological testing is performed according to USP standards, with incubation periods longer than the minimum criteria to confirm the absence of pathogens.
All test data is digitally archived permanently with complete batch traceability. We provide our customers with complete documentation packages that include stability study results and a Certificate of Analysis that has been verified by our quality management personnel.
Flexible Supply Chain and Delivery Options
Direct Factory Pricing
Eliminate unnecessary middleman costs to the manufacturer. Bulk pricing for annual supply agreements and repeat orders that is competitive.
Configurable Order Quantities
Standard packing 25kg fibre drums double layer food grade polyethylene lining. Flexible MOQ options for trial formulation development and high volume commercial production.
International Delivery Terms
We have a variety of Incoterms such as EXW, FOB, CFR, CIF, DAP and DDP to meet your logistics needs. Sea freight, air transportation and rapid courier services ensure quick delivery worldwide.
Ways to Pay
For your convenience and transaction security, we accept 100% T/T bank transfer, Alibaba International Trade Assurance, Western Union.
FAQ
Q: How do you ensure consistent quality across different production batches?
A: Each batch undergoes full inspection via HPLC assay, heavy metal analysis, and comprehensive microbiology testing before warehouse release. All test data is recorded in our quality management system with complete traceability, guaranteeing consistent ≥98% purity specification across all lots.
Q: Can your facility adapt particle size for different manufacturing equipment?
A: Yes, we adjust particle fineness to fit your specific filling and compression machines. Whether you're producing softgels, tablets, or capsules, our technical team will optimize powder characteristics to ensure smooth production flow and uniform content distribution.
Q: What is the typical lead time for orders?
A: In-stock inventory orders ship within 3-5 business days after payment confirmation. Bulk orders or high-purity custom specifications require 10-12 days for production and quality verification.
Q: Which industries commonly use this ingredient?
A: Widely applied in dietary supplement manufacturing, functional food development, metabolic health product formulations, and specialized nutrition beverage systems. The ingredient serves both nutraceutical-grade and food-grade application requirements.
Q: What storage conditions prevent quality degradation?
A: Store in fully sealed containers away from direct light and heat sources. Maintain cool, dry warehouse conditions with controlled humidity. Avoid prolonged high-temperature exposure which may cause gradual discoloration without affecting chemical purity.
Partner With a Trusted Manufacturer
Contact our team at enquiry@lenutra.com to request Benfotiamine Powder samples, discuss custom specifications, or receive detailed technical documentation for your formulation projects.
Online Message
YOU MAY LIKE
High-quality Botanical Extracts, Functional Ingredients, And Nutraceutical Raw Materials Manufacturer And Supplier